EMAIL US:salesmanager@singi.com
- All
- Product Name
- Product Keyword
- Product Model
- Product Summary
- Product Description
- Multi Field Search
Views: 1 Author: Mark Zhang Publish Time: 2026-11-19 Origin: 本站
A mid-sized electrical equipment manufacturer in Southeast Asia produces compact distribution boards, DIN-rail terminal blocks, and control enclosures for commercial buildings. The company runs two plants, employs 420 people, and ships 180,000 assemblies a year. Growth brought tighter delivery windows and more demanding incoming inspection from panel builders. One component family kept causing trouble: the plastic shell metal parts that hold terminals, guide contacts, and anchor mounting brackets inside low-volt-level assemblies.
The manufacturer serves system integrators and electrical contractors across Southeast Asia. Orders are small to mid-volume, with many variants. A typical distribution board uses several plastic shell metal parts: terminal carriers, contact brackets, and mounting inserts. The parts must fit into molded housings, accept screw torque, and hold alignment through assembly and transport.
Market pressure came from two directions. Panel builders wanted shorter lead times and lot-level traceability. End users wanted assemblies that pass routine dielectric and temperature-rise checks without rework. The manufacturer had capacity, but variation in one purchased component family slowed final assembly and raised inspection costs.
The company bought stamped metal inserts from one supplier and molded plastic shells from another. Assembly teams pressed the inserts into the shells on a manual line. The approach worked at low volume. At higher volume, three problems surfaced.
First, insert position drifted. Plastic shrinkage varied by lot, and the stamped parts had slight burr differences. When the two tolerances stacked, inserts sat off-center. Operators forced them into place, which cracked the shell or loosened the contact seat. The assembly reject rate reached 4.8%.
Second, plating wear caused field failures. Metal inserts were barrel-plated before shipment, then handled again during pressing. Scratches exposed base metal on some lots. In humid installations, contact resistance rose. The manufacturer logged 11 customer complaints in one year tied to terminal heating and intermittent contact.
Third, supplier coordination consumed engineering time. Five vendors covered different shell sizes and metal inserts. Each change required separate drawing reviews, sample approvals, and incoming inspections. Purchasing held 35 days of lead time and 22 days of safety stock. On-time delivery from the component chain averaged 82%.
The direct costs were visible: $86,000 a year in rework and scrap, $34,000 in expedited freight, and 600 engineering hours spent on supplier corrective actions. The less visible cost was line stability. Final assembly output moved by 15% week to week because teams never knew how many shells would pass the press-fit station.
The manufacturer reviewed three options. One was to keep separate sourcing and tighten incoming inspection with 100% gauging. That added two inspectors per shift and did not address handling damage. Another was to reshore the metal stamping and mold the shells in-house. The capital estimate exceeded $420,000 and would take nine months. The third was to buy integrated plastic shell metal parts from a supplier that controls molding, stamping, plating, and assembly in one process.
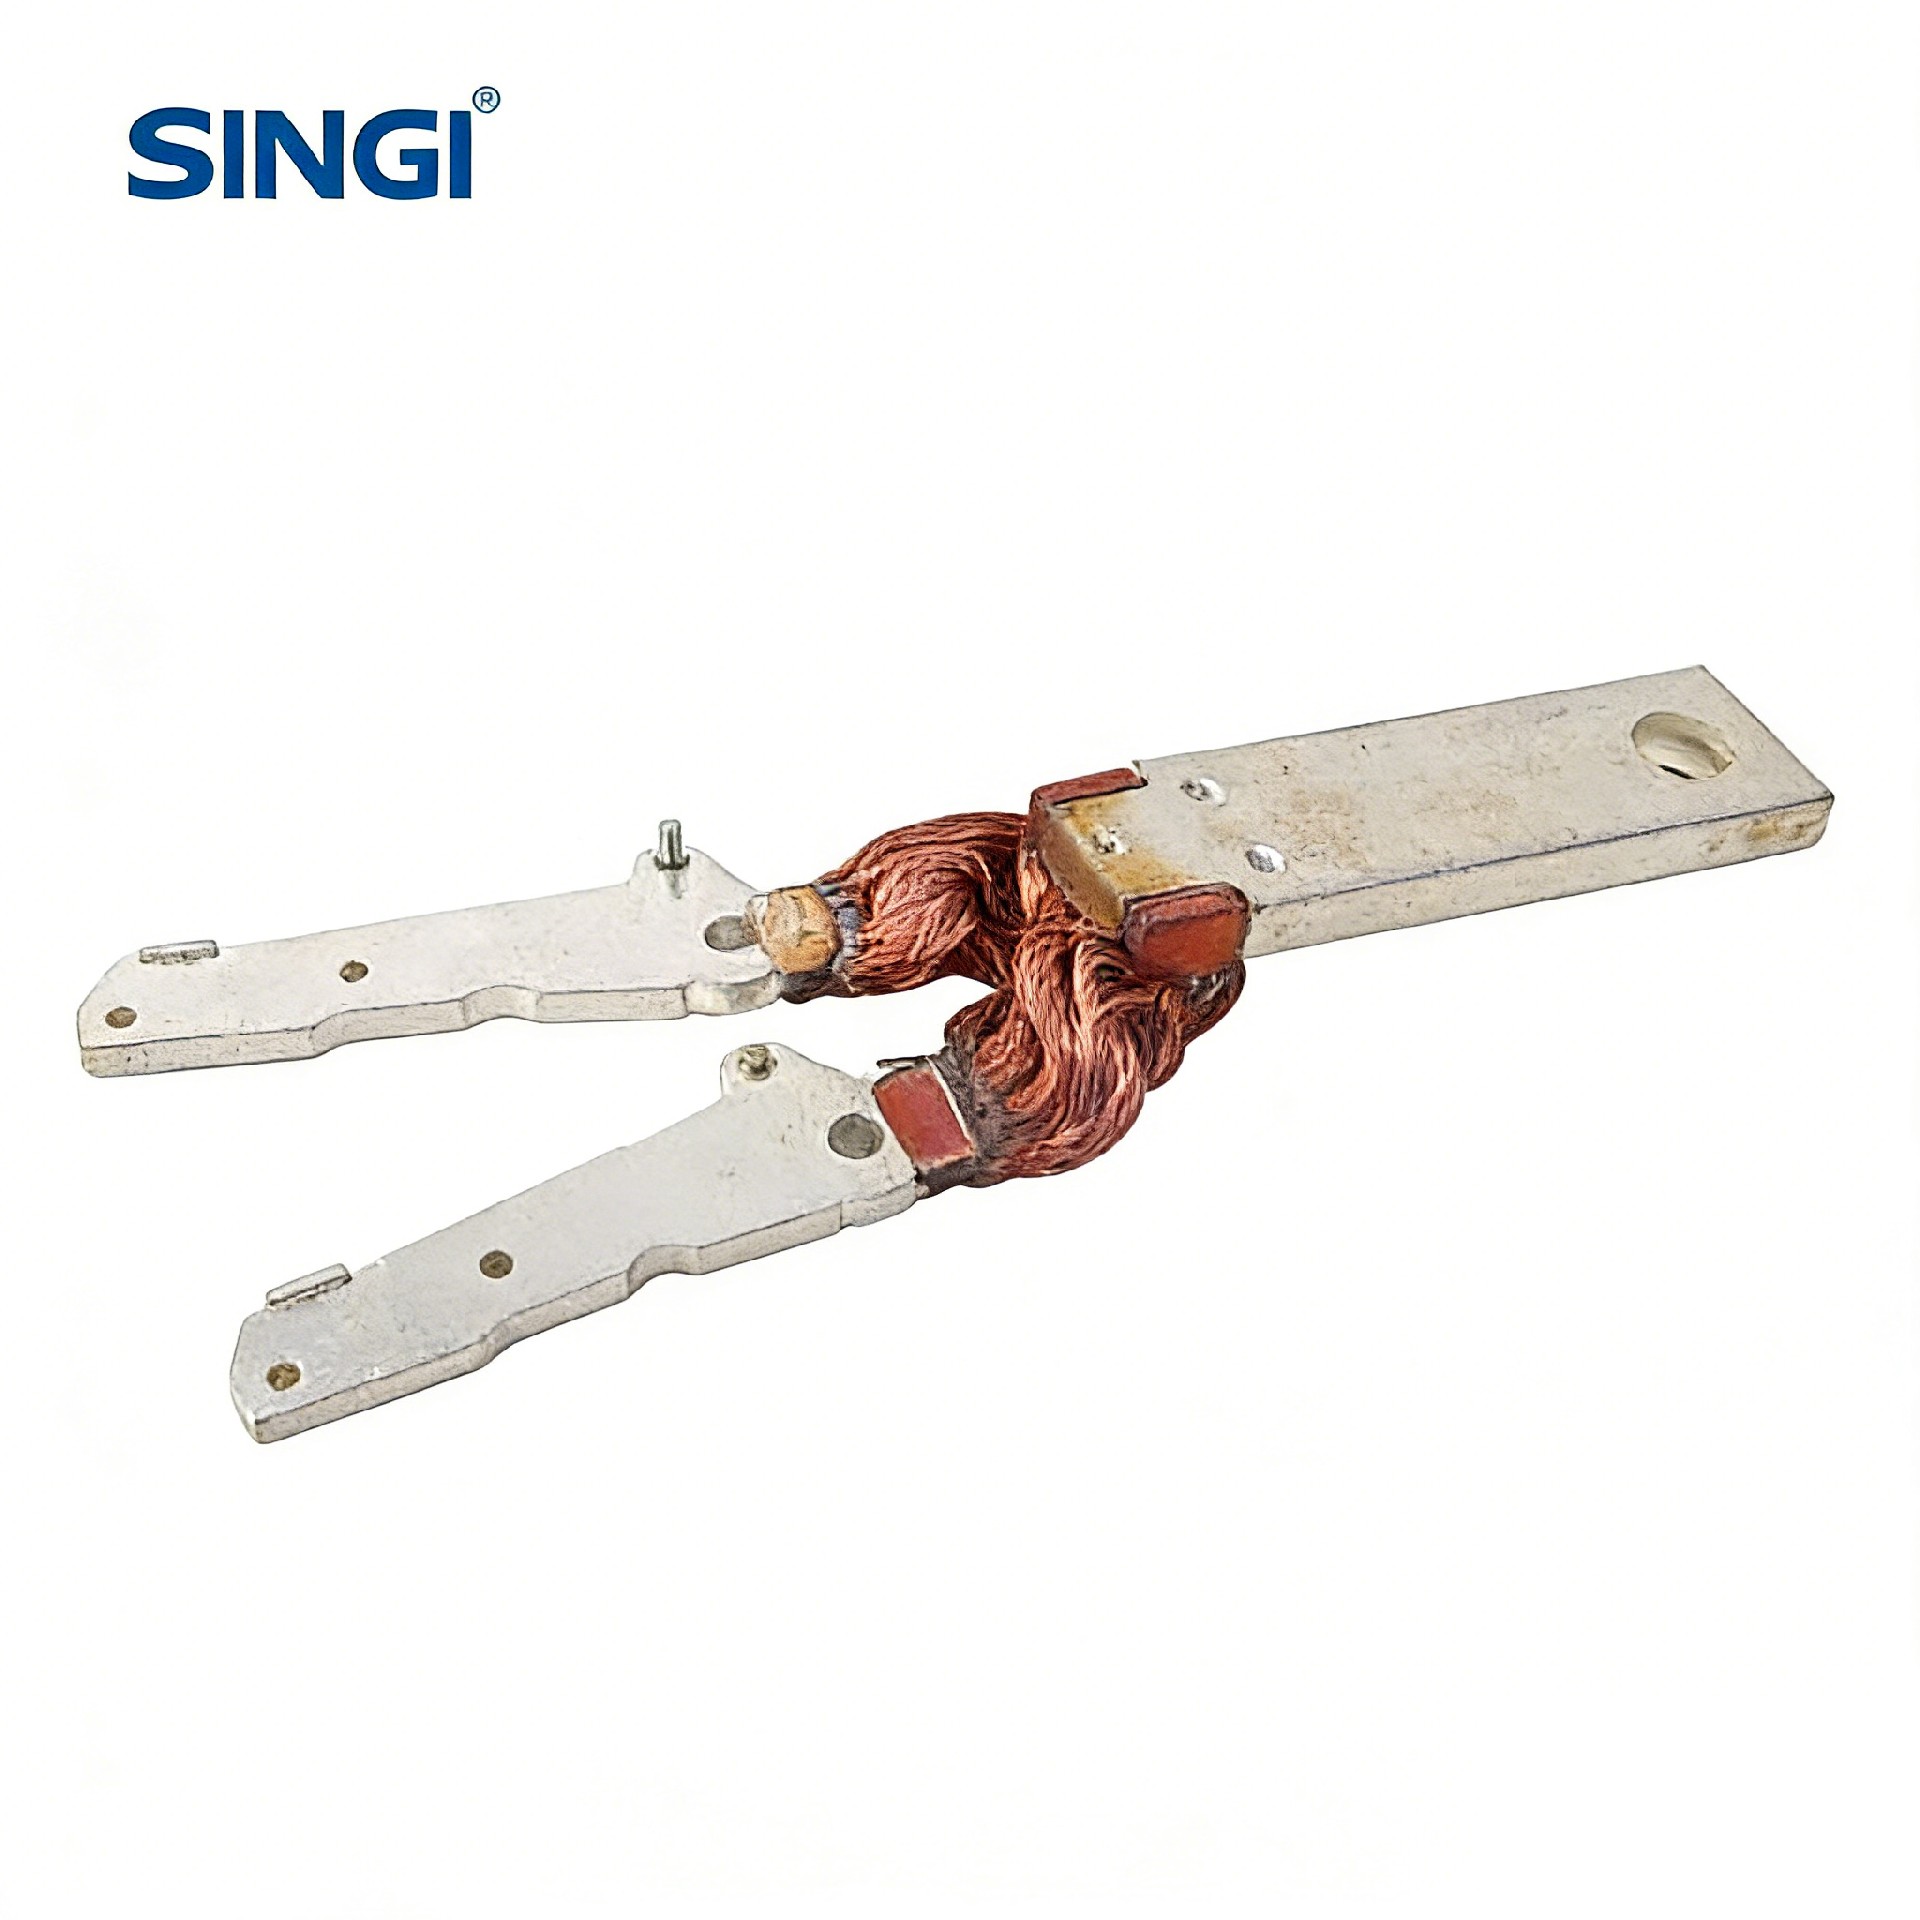
SINGI plastic shell metal parts matched the third path. The parts combine molded plastic shells with metal inserts, terminals, and brackets in one controlled assembly. Key reasons for choice:
Engineering compared first articles against IEC 60947-1 general rules for low-volt-level switchgear and controlgear, clearance, creepage, and mechanical durability checks used in the customer’s component qualification. The integrated part passed the 500-cycle insertion test and the 1.2 N·m screw torque test without shell cracking.
The project ran for 12 weeks from kickoff to production release. The first two weeks covered drawing review and a tolerance study on three high-volume part numbers. The manufacturer shared assembly fixture drawings and torque data. SINGI proposed minor rib changes to guide the insert during overmolding and a masked area on the contact face to protect plating.
Weeks three to six covered tooling build and first article inspection. Samples were measured on a coordinate measuring machine for insert position, shell flatness, and terminal height. Plating thickness was checked on coupons from the same run. Weeks seven to nine covered a 2,000-piece pilot on the customer’s press-fit line. Weeks ten to twelve covered process capability review, packaging approval, and production ramp.
The main difficulty appeared in the pilot. One shell variant showed a 0.18 mm insert shift after molding. The shift was inside the drawing tolerance but outside the customer’s assembly fixture allowance. SINGI ran a mold flow review, adjusted gate location, and added a post-mold cooling fixture. The next lot held insert position within 0.08 mm. The customer also modified one assembly nest to stop over-compressing the shell during pressing.
After three months of production, the manufacturer measured results across the three part families:
Final assembly output variance narrowed from 15% to 4% week to week. Customer complaints tied to terminal heating dropped to zero in the first two quarters after release. The manufacturer also passed a panel-builder audit without a minor finding on insert alignment or plating traceability.
“The parts arrive ready for the line,” said the production engineering manager. “The team stopped chasing insert position and plating damage. The first pilot lot showed the mold needed a cooling fixture, and the supplier fixed it without pushing the launch date.”
He added: “The cost saving is real, but the bigger gain is that final assembly is predictable. The plant can quote shorter lead times because it is not rebuilding shells at the end of the month.”
1. Qualify plastic shell metal parts as one assembly, not as separate plastic and metal purchases. Check insert position, pull-out force, torque strength, and plating thickness on the same lot. A part that passes a metal drawing can still fail when molded into a shell.
2. Share the assembly fixture early. Tolerance stack-up belongs to the line, not the drawing. A 0.18 mm shift may pass inspection and still stop a press-fit station. Send nest drawings and torque settings during quoting.
3. Keep lot traceability from resin and metal coil through plating. For low-volt-level switchgear components, IEC 61439-1 assembly checks depend on repeatable contact and clearance dimensions. Traceability shortens root-cause work when a lot drifts.
If the project were repeated, the manufacturer would run a capability study on the customer’s press-fit nest before mold release. That step would have caught the cooling issue earlier and avoided one pilot rework loop.